

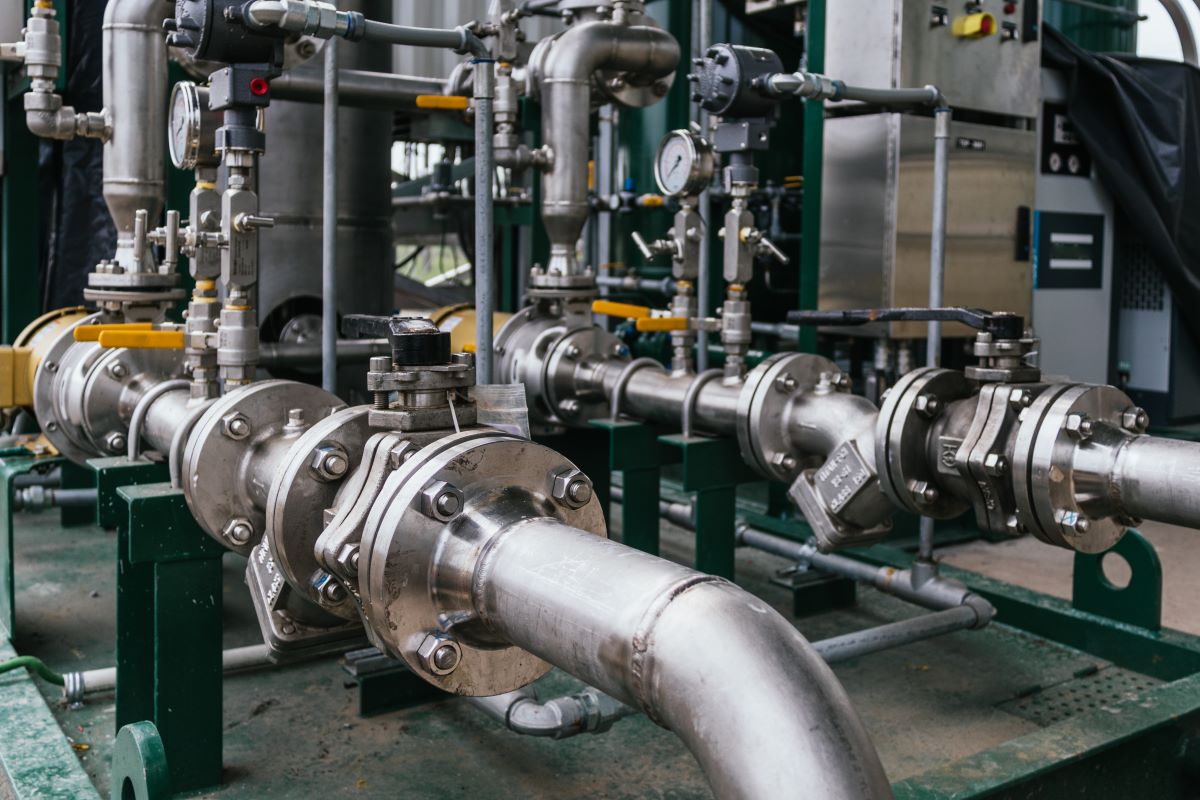

A safety valve protects pressurized equipment by releasing fluid when pressure reaches a predetermined level. This article explains how safety valves work, their main components and types, common applications, and the importance of correct selection and regular maintenance.
A safety valve protects pressurized equipment by automatically releasing fluid when pressure reaches a predetermined level. From steam boilers and compressed air receivers to industrial process vessels, these devices help limit overpressure that could otherwise damage equipment and endanger personnel.
Pressure can increase unexpectedly when an outlet becomes blocked, a control component fails, or operating conditions change. An effective protection system must account for these situations before they occur.
Understanding how safety valves operate, where they are used, and what influences their selection helps businesses make informed equipment decisions. It also explains why correct installation and maintenance deserve as much attention as the valve itself.
What Is a Safety Valve?
A safety valve is an automatic pressure relief device commonly associated with steam, gas, and other compressible fluids. It opens when inlet pressure reaches its specified set pressure, providing a discharge path that helps protect the connected equipment.
Unlike a control valve, which continuously adjusts process conditions, a safety valve serves a protective function. It should not routinely compensate for unstable pressure control or become part of normal production regulation.
Its effectiveness depends on more than opening at the correct pressure. The valve must also discharge sufficient fluid for the identified overpressure scenario. A correctly calibrated valve with inadequate relieving capacity may still leave equipment insufficiently protected.
How Does a Safety Valve Work?
In a conventional spring-loaded design, a compressed spring applies force to a disc, holding it against the valve seat. Pressure from the protected system acts beneath the disc in the opposite direction.
During normal operation, the spring maintains the seal. As pressure rises toward the set point, the opening force increases. At the specified opening condition, the valve begins to lift. Many safety valves intended for compressible fluids then open rapidly through a characteristic “pop” action.
The resulting flow carries fluid away from the protected equipment. The valve must achieve its required relieving capacity within the pressure limits permitted for the application.
Once pressure falls sufficiently, the spring returns the disc to its seat. The difference between set pressure and reseating pressure is called blowdown.
Discharged fluid must travel to an appropriate destination. Depending on the medium and installation, this may involve a suitably designed vent, collection arrangement, or closed discharge system.
Main Components of a Safety Valve
Although construction varies, a conventional spring-loaded valve contains several essential components.
The body forms the pressure-containing housing and connects the inlet and outlet. Its material must suit the fluid, temperature, and service environment.
The nozzle and seat define the inlet passage and sealing surface. The disc closes against the seat during normal operation and lifts to permit discharge.
The spring provides the closing force, while the spindle transmits force and guides movement. The bonnet houses the spring assembly, with its configuration depending on service requirements.
Some models include a lifting lever or a bellows assembly. These features serve specific purposes and should be selected according to the application. A lifting lever, for example, does not replace a documented inspection and testing programme.
Common Types of Safety Valves
Different operating conditions require different valve designs. Three widely encountered arrangements are conventional spring-loaded, balanced bellows, and pilot-operated valves.
Conventional spring-loaded valves use a spring to hold the disc closed. Their relatively straightforward construction makes them suitable for many applications, provided operating conditions remain within the design’s limitations.
Balanced bellows valves incorporate a bellows arrangement that reduces the influence of back pressure on specified performance characteristics. Depending on construction, the bellows can also help isolate certain internal components from the process fluid.
Pilot-operated valves use a pilot device to control the main valve. Some designs offer advantages where operating pressure is relatively close to set pressure or where application conditions favour pilot control.
No design is universally preferable. Fluid cleanliness, temperature, pressure variation, back pressure, and maintenance requirements all influence suitability. The final choice should follow the manufacturer’s documented operating limits.
Where Are Safety Valves Used?
Safety valves are used wherever a credible overpressure event could exceed the permitted limits of pressurized equipment. Common examples include steam boilers, compressed air receivers, process vessels, and equipment downstream of pressure reducing stations.
In a steam installation, failure of an upstream pressure reducing valve may expose downstream equipment to excessive pressure. The protective device must be selected for the resulting fault flow, rather than only the normal steam demand.
Industrial applications also include chemical processing, food production, energy generation, and manufacturing utilities.
The location of the protective device matters. Its connection must allow it to sense the pressure requiring protection and relieve the necessary flow. Inlet restrictions and unsuitable discharge piping can undermine an otherwise appropriate valve selection.
What Is the Difference Between a Safety Valve and a Relief Valve?
The terms are sometimes used interchangeably, but their technical meaning can differ.
In common industry terminology, a safety valve typically serves compressible fluids and exhibits rapid opening. A relief valve is generally associated with liquid service and opens progressively as pressure increases. A safety relief valve may be suitable for either function, depending on its design and approval.
This distinction reflects differences in fluid behaviour. Compressed gas and steam store energy differently from liquids, influencing the required opening characteristics and capacity assessment.
However, terminology varies between standards, industries, and manufacturers. A product name alone does not establish suitability.
Engineers should verify the valve’s approved fluid service, certified capacity, pressure and temperature limits, and applicable design requirements. Substituting one valve for another without reviewing these details can create performance problems even when the connections appear identical.
How to Choose the Right Safety Valve
A safety valve supplier should be able to support selection with clear technical documentation and application-specific information. Buyers should provide the fluid, operating conditions, equipment pressure limits, required relieving capacity, and expected back pressure.
Selection should address credible failure scenarios rather than rely solely on pipe diameter. An oversized valve can also create operating difficulties, including unstable cycling.
Material compatibility, connection ratings, discharge arrangements, and relevant certification require review before purchase. Documentation should identify the supplied valve and its specified settings.
The strongest purchasing decisions connect process requirements with verified product performance. This gives engineering and maintenance teams a clear basis for installation, inspection, and future replacement.
Why Regular Safety Valve Maintenance Matters
Service conditions can affect performance over time. Deposits, corrosion, seat damage, and mechanical wear may cause leakage, restrict movement, or prevent reliable reseating.
A planned maintenance programme should reflect the fluid, operating history, manufacturer’s instructions, and applicable inspection requirements. There is no single interval suitable for every installation.
Records should document inspections, test results, repairs, and relevant operating events. Persistent leakage or repeated lifting warrants investigation of both the valve and the surrounding process.
Testing, adjustment, and repair should be performed by appropriately qualified personnel using suitable procedures. Manufacturer guidance likewise calls for planned maintenance and authorized setting work.
Reliable pressure protection depends on correct selection, installation, and continued care throughout the equipment’s working life.